 АНГЛИЙСКИЙ
 EN
 RU
 ES
 KO
 JA
 PT
 IT
 DE
 FR
 NL
Быстрые ссылки
In brief: source custom commemorative coin presentation boxes by treating the coin, capsule, insert, certificate, rigid box and export pack as one controlled system. Give every shortlisted manufacturer the same specification, approve fit before decoration, define measurable defects before production, and compare quotations on equivalent materials, tooling, packing and delivery terms. MOQ, sample timing and unit price should be confirmed against the final construction rather than borrowed from a generic box listing.
This guide is for mints, numismatic publishers, museums, recognition-program managers and packaging buyers purchasing paper-wrapped rigid boxes in volume. It does not cover stock velvet cases, wooden cases or archival coin storage. If you are still choosing a structure, start with the rigid coin box style guide; this article begins when you are ready to request samples and commercial quotations.
A quote is only comparable when suppliers are pricing the same deliverable. “Premium coin box” is not a specification: one supplier may quote a paper-wrapped hinged box with a die-cut foam insert, another a folding carton, and another a stock case with a printed sleeve. Their prices may all be reasonable, but the comparison is meaningless.
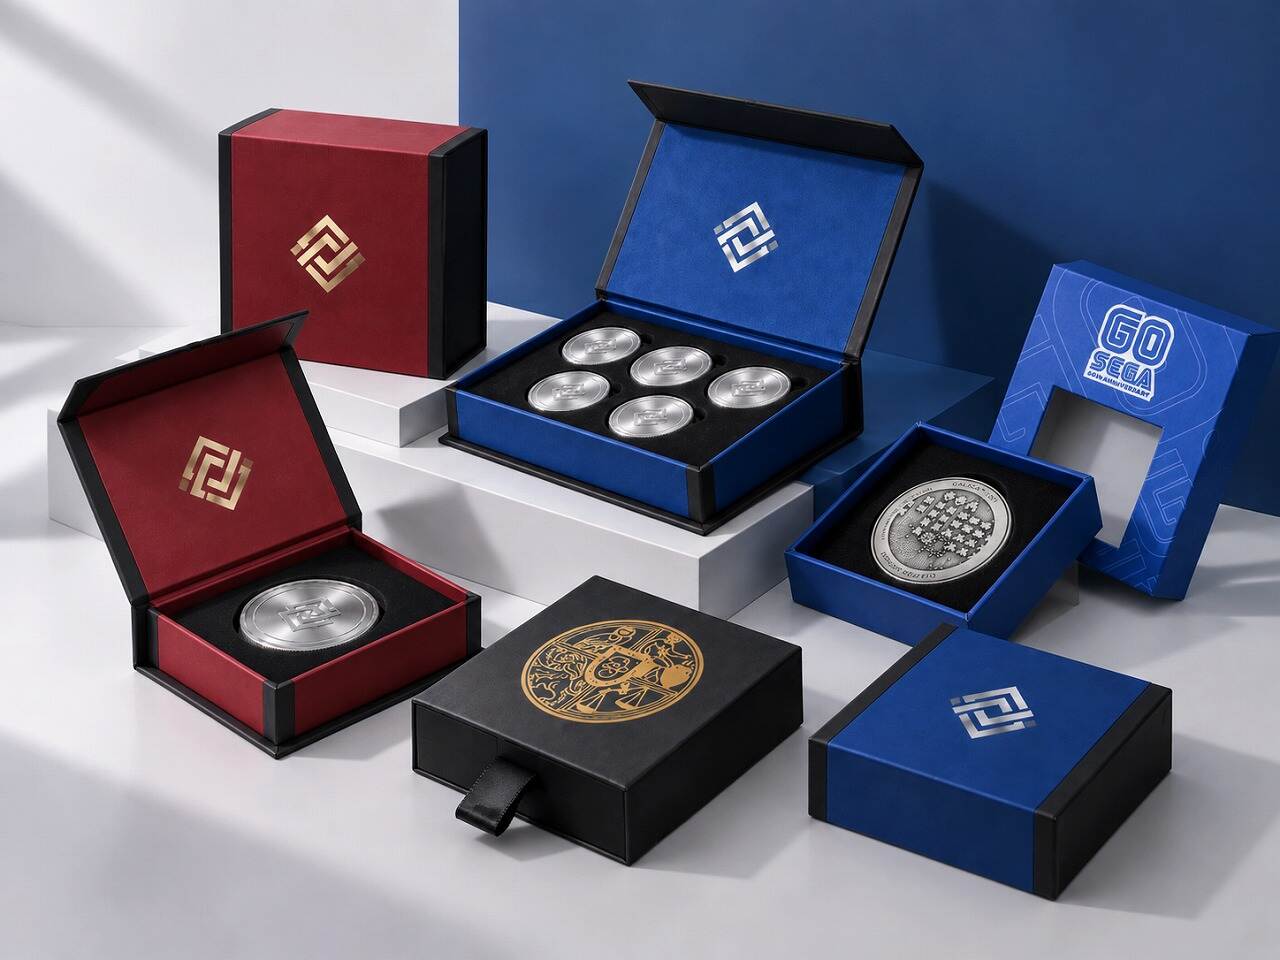
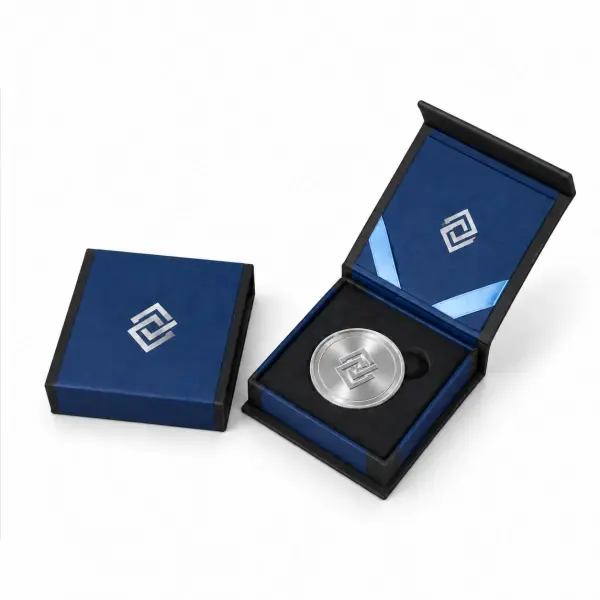
Start with the program and packed item. State whether the box is for a single proof coin, a multi-coin commemorative set, a medal, a challenge coin or a graded slab. Identify the holder as a bare coin, clear capsule or slab and provide its maximum outside dimensions. Then define the opening style, certificate position, branding, unit pack and route to market. The custom commemorative coin presentation box page shows how these inputs connect in one product brief.
| Purchase question | Controlled input | What goes wrong if omitted |
|---|---|---|
| What is being packed? | Physical capsule, slab or medal plus maximum dimensions and weight | Insert and outer size are guessed |
| How is it presented? | Orientation, visible face, removal method and certificate position | The reveal looks wrong or the item is difficult to remove |
| How is it sold? | Retail, institutional issue, direct-to-consumer parcel or distributor shipment | Barcode, label, sleeve and outer-pack needs appear late |
| How is success judged? | Approved sample, drawing, color target and written acceptance criteria | Approval becomes subjective after production |
Commercial boundary: a premium rigid box is presentation packaging and secondary mechanical protection. It should not be sold as airtight, corrosion-proof or archival unless the complete holder, contact materials and storage system have evidence for that claim.
A good RFQ reduces interpretation without over-engineering the solution. Separate fixed requirements from preferences and supplier recommendations. For example, the capsule outside diameter and certificate size may be fixed, while insert material can remain “supplier to recommend and justify.” That gives capable manufacturers room to improve manufacturability without changing the buying brief.
Physical samples or controlled drawings, maximum envelope, weight, capsule rim profile, set count, orientation and removal requirement.
Preferred box style, target footprint, insert concept, certificate compartment, outer sleeve and any retail labeling area.
Print-ready artwork, color references, wrap sample, foil reference, emboss or deboss file, inside copy and certificate revision.
Quantity by design, total quantity, delivery destination, target date, Incoterm, inspection request and packing requirements.
Ask each supplier to return a specification summary with assumptions and exclusions. The summary should identify proposed materials, finished dimensions, print and finish processes, insert construction, sample route, one-time tooling, unit packing and quotation validity. GPLPAK's design validation for manufacturing page describes the point at which a creative concept is checked against production methods and price options.
There is no responsible universal MOQ for every custom coin box. The commercial minimum is created by the chosen processes: printed sheets, specialty-paper purchase, greyboard conversion, insert sheets, dies, foil plates, setup time, assembly and packing. A supplier may accept a small run but allocate the same setup cost across fewer units, which raises the unit price. Another may require a larger batch because a specific material or process is purchased in production lots.
| Cost driver | Why it changes the quote | Buyer action |
|---|---|---|
| Size and structure | Board, wrap area, components and assembly steps change | Request a costed alternative only if the packed-item fit remains controlled |
| Insert construction | Material, thickness, cutting, covering and bonding vary | Compare function and appearance, not material names alone |
| Decoration | Foil, embossing, spot gloss and interior print add setup and registration work | Set a finish hierarchy and remove processes that do not add buyer value |
| Artwork splits | Multiple dates, languages or serial panels reduce run efficiency | State quantity per version and identify shared components |
| Pack-out and freight | Unit protection, master-carton quantity and shipment volume affect landed cost | Compare packed dimensions, carton plan and Incoterm with the unit price |
Request quantity breaks based on the same specification. Keep one-time charges separate from recurring unit cost and ask who owns or stores each die, plate and fixture. For a broader breakdown of structure and finish variables, see how custom rigid box cost is built.
Normalize the commercial comparison before selecting a supplier. Convert every offer to the same currency, quantity, pack-out and named delivery basis; then add sample charges, tooling, inspection, estimated freight, import costs and any local fulfillment work that is outside the quoted scope. Record whether overrun or underrun quantities are permitted and how they are invoiced. A slightly higher unit price may produce a lower landed program cost when the quotation includes better unit protection, fewer separate tools or a reusable structure for later editions. Conversely, a low unit figure can be misleading when certificates, sleeves, inner cartons or export pallets are excluded.
Sampling is most efficient when each stage has a defined decision. Do not pay for a fully decorated sample while the capsule cavity, lid clearance and certificate insertion sequence are still changing. Prove fit first, then appearance, then the production-intent combination.
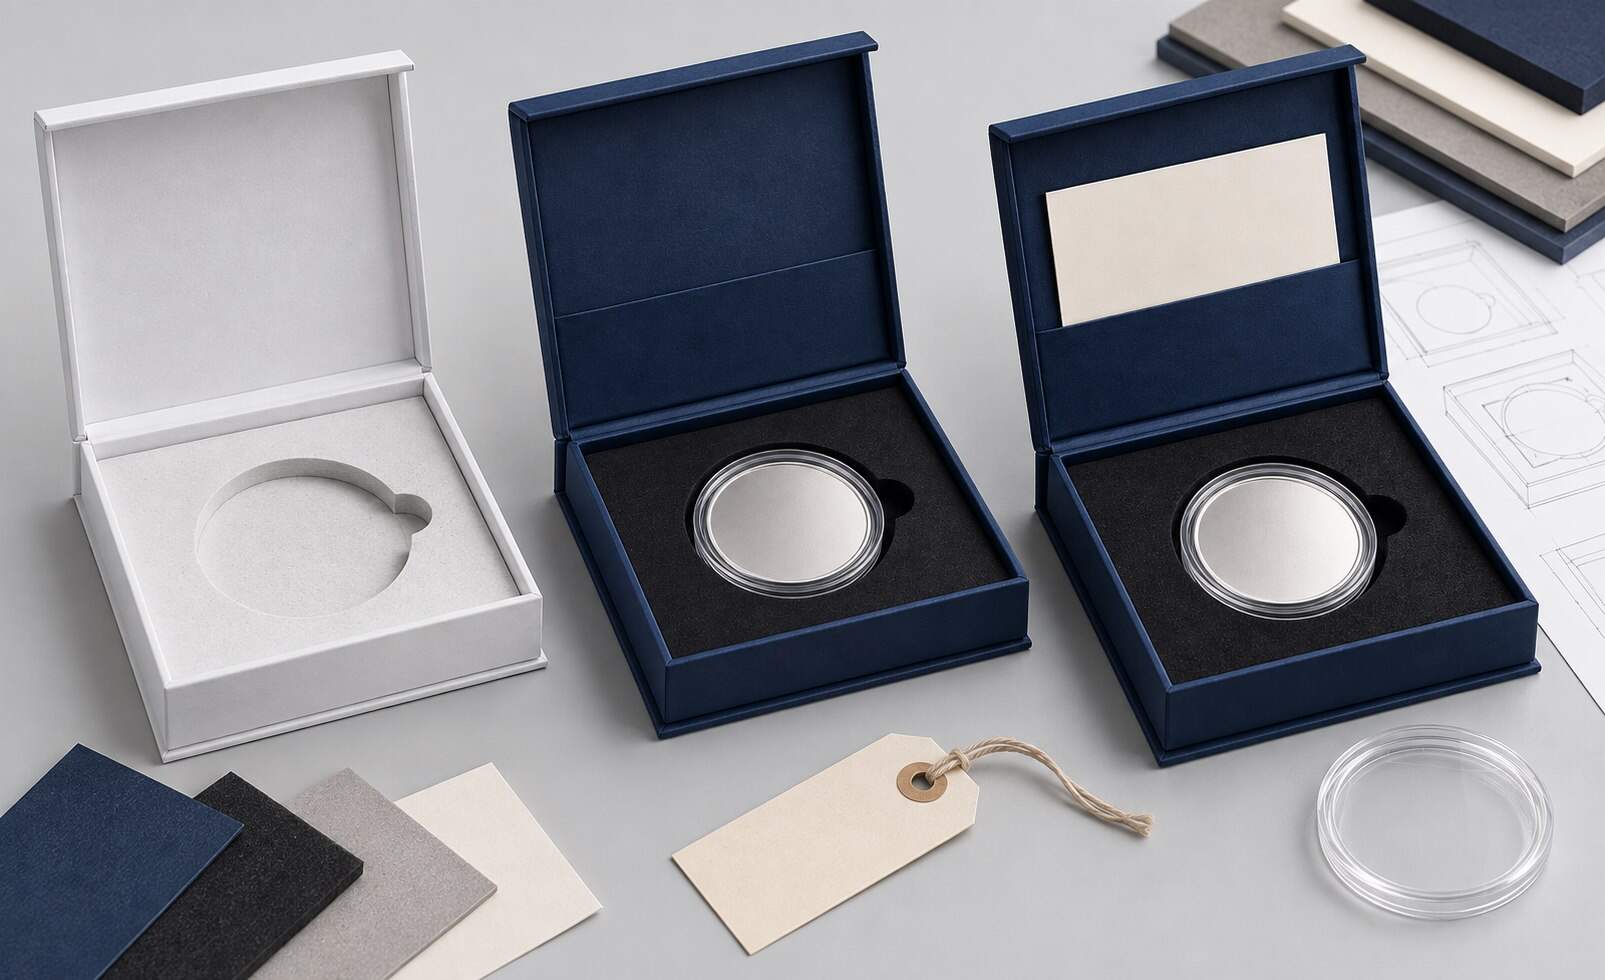
Separate structural, appearance and production-intent approvals so a late visual change does not hide an unresolved fit problem.
| Sample stage | Primary decision | Do not assume it proves |
|---|---|---|
| Digital or 3D concept | Layout, hierarchy and approximate proportions | Physical fit, paper behavior or production color |
| Plain structural mock-up | Dimensions, opening action, cavity and removal method | Final print, foil shade or surface character |
| Appearance proof | Artwork scale, material character and finish positions | Mass-production repeatability if processes differ |
| Production-intent sample | Complete packed system and approval reference | Every unit will be identical without written tolerances and inspection |
Record what each sample is made from, which processes differ from production and which revision it represents. Approve the sample with dated notes, not a message that says only “looks good.” GPLPAK's выборка развития page explains how plain, printed and process-representative samples support production decisions.
For a new construction, agree how the first production units will be reviewed before the entire lot is completed. This may be a start-of-run check, a retained production reference or a staged release, depending on schedule and process. The purpose is not to reopen approved design choices; it is to catch setup errors such as the wrong artwork plate, reversed certificate orientation, incorrect insert depth or finish registration before those errors repeat across the lot. State who may approve a correction and whether work must pause while approval is pending.
Quality control begins with defect definitions, not with an inspector arriving at the end of production. The purchase specification should state what is checked, how it is measured, what reference controls the decision and what happens when the result fails. Separate safety, function, identity and cosmetic appearance so that every issue is not treated as equally serious.
| Defect class | Coin-box example | Control method |
|---|---|---|
| Critical | Wrong coin identity, missing required certificate, prohibited sharp part or incorrect mandatory copy | Explicit zero-tolerance requirement where appropriate and traceable version check |
| Major | Capsule will not seat, coin can escape, lid will not close, insert is detached or artwork is materially wrong | Functional gauge, physical test and approved artwork comparison |
| Minor | Small cosmetic variation within an agreed viewing condition and limit | Signed visual standard, defined lighting and viewing distance |
If you use acceptance sampling, name the plan, edition, lot definition, inspection level and acceptance values in the purchase agreement. ISO 2859-1:2026 defines AQL-indexed sampling schemes for lot-by-lot inspection. The standard helps decide how a sample represents a lot; it does not write your product specification, define which defects matter to your brand or replace process control.
Approval rule: attach the approved sample, drawing, artwork revision, material references and defect list to the purchase order. An isolated sample on a video call is not a complete quality agreement.
The same finished unit should be inspected in a logical sequence. Begin with identity and count, then dimensions and fit, then operation, then decoration and cosmetic appearance. This order prevents a beautiful surface from distracting attention from a box that does not actually hold the capsule correctly.
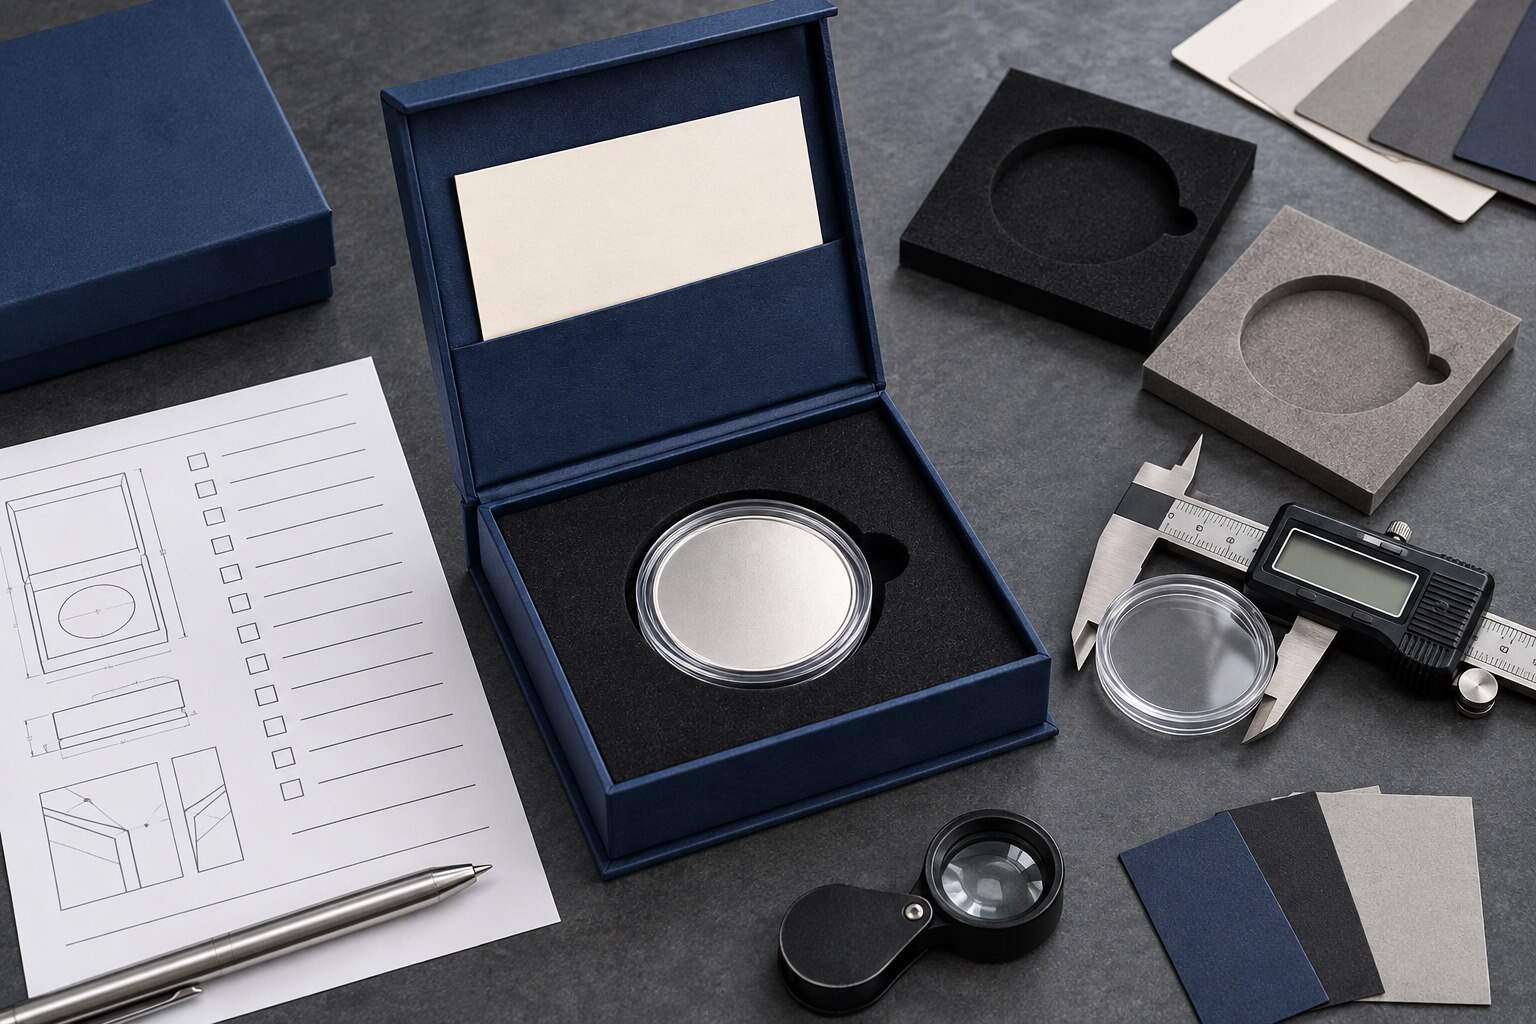
A useful inspection connects each acceptance point to a tool, sample, drawing or approved visual reference.
Verify the capsule or slab against the approved production component, not a similar sample.
Check seating, movement under agreed handling, finger access or ribbon lift, and clearance when the lid closes.
Operate the lid, drawer or sleeve through the agreed cycles and assess alignment, binding and closure behavior.
Confirm certificate count, orientation, insertion and removal without bending or interfering with the coin.
Compare print to the approved proof or color target under agreed lighting.
Review foil registration, filling, pinholes and edge definition against a signed limit sample.
Inspect wrap alignment, turned edges, corner formation, glue contamination, scuffing and board exposure.
Confirm that all artwork and certificate versions match the packing list for that lot.
Where a dimension is critical, put the measurement location and method on the drawing. “Box size” is ambiguous unless it says internal or external dimensions and identifies the orientation. The box measurement guide provides a useful shared vocabulary for quotations and inspection.
The presentation box is not automatically the shipping package. A paper-wrapped rigid surface can be scuffed by neighboring units, corners can be compressed inside an under-filled carton, and a heavy multi-coin set can overload an insert or divider. Define the pack-out at the same time as the box, then quote it as part of the system.
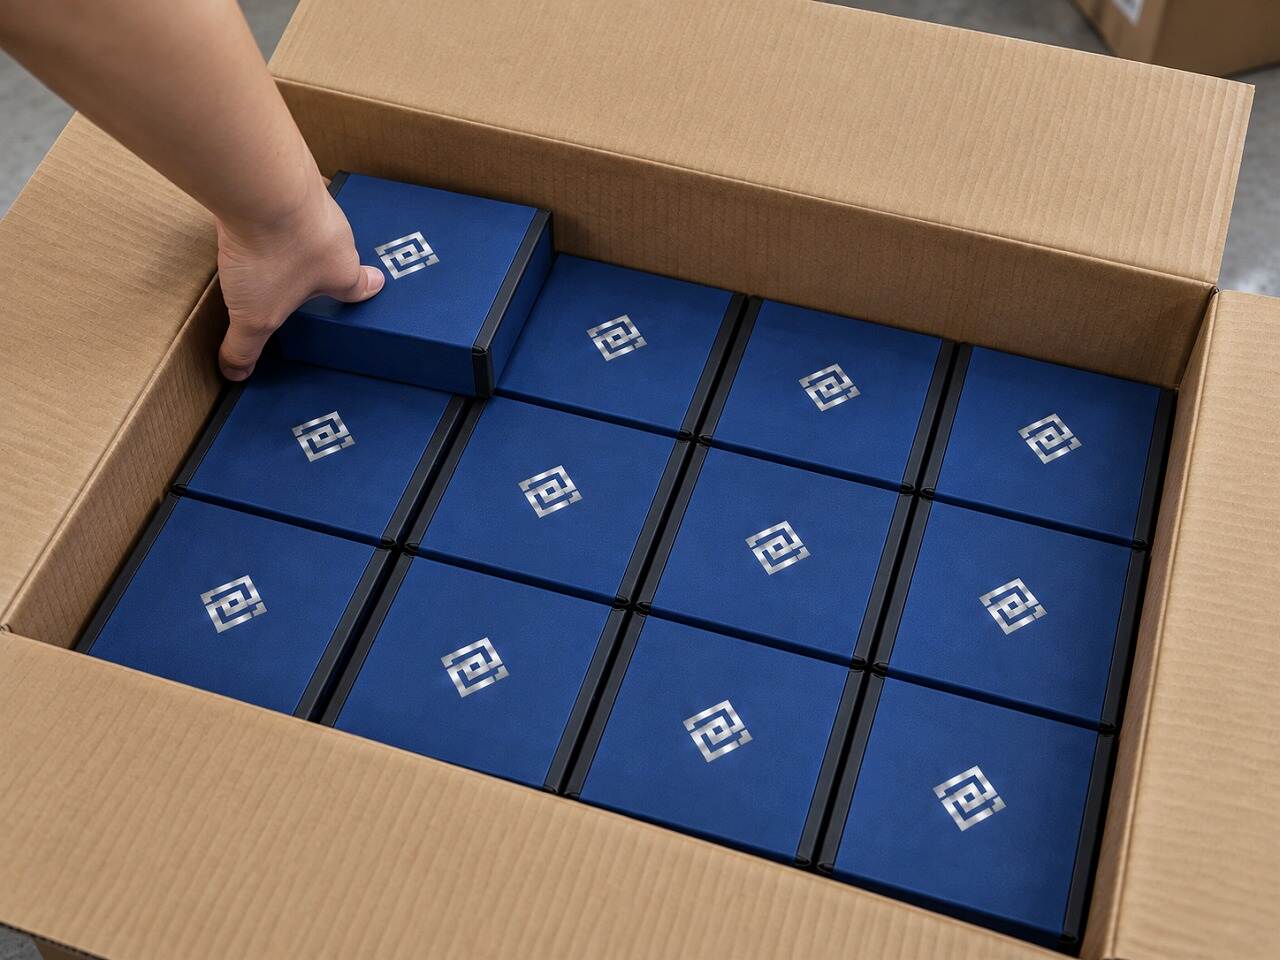
Unit sleeves, dividers, void control and carton quantity should be approved as part of the packed system.
Unit protection: agree tissue, sleeve, bag, corner protection or interleaf material and whether it may contact printed or specialty surfaces.
Case configuration: define units per carton, orientation, divider pattern, void fill, carton closure and maximum packed weight.
Pallet or parcel route: identify whether cartons move by parcel, mixed freight, full-load distribution or direct import, because hazards and handling differ.
Acceptance after testing: define acceptable coin movement, box scuffing, corner deformation, certificate condition and shipper damage before the test.
ISTA distinguishes screening procedures from partial and general simulations, and its procedure selection guidance starts with the actual distribution environment. The current ISTA procedure descriptions also make clear that the package and product are evaluated together. A factory drop demonstration or an empty-box test is not equivalent to a documented ISTA test of the representative packaged product.
If certification or use of the ISTA Transit Tested Mark is required, discuss it with a qualified laboratory before testing. ISTA states that it certifies a qualifying packaged product for the shipper member, not a generic package for a packaging supplier. GPLPAK's packing serviceиcorrugated box pages provide the related pack-out context.
Ask for a carton data sheet after pack-out approval. It should identify finished carton dimensions, gross and net weight, units per carton, carton count, pallet pattern where applicable and the protective materials inside. Those values let your forwarder price the actual shipment and help the receiving team plan handling and storage. If transport mode or delivery channel changes after approval, review whether the carton, dividers and test basis still represent the new route rather than assuming the original pack-out remains suitable.
“Premium,” “high quality” and “experienced” do not show whether a supplier can control your specific box. Ask for project evidence: a dimensioned proposal, material samples, a clear sample route, process-appropriate tolerances, inspection records and a pack-out plan. A capable manufacturer should identify missing information and explain trade-offs rather than promise every option immediately.
| Evaluation area | Useful evidence | Supplier warning sign |
|---|---|---|
| Engineering | Controlled drawing, cavity logic, removal method and assumptions list | Quote based only on coin diameter or a photograph |
| Sampling | Stage purpose, materials, deviations, timing and approval record | A sample is presented as production-equivalent without stating differences |
| Quality | Inspection points tied to drawing, artwork and approved standards | Only “100% quality guaranteed” with no method or limits |
| Commercial clarity | Itemized tooling, unit price, pack-out, validity, exclusions and Incoterm | Low headline price with material, packing or delivery basis omitted |
| Change control | Revision log and written approval before substitutions | Verbal substitutions or uncontrolled artwork files |
A factory visit or audit can confirm relevant processes, but the audit scope should match the order. For rigid coin boxes, useful observations include greyboard conversion, wrapping, hinge formation, insert cutting or covering, assembly, inspection and packing. Do not treat an unrelated automated line or a certificate image as proof of capability for your construction. See GPLPAK's factory services for the separation between sampling, manufacturing and packing activities.
Also evaluate response quality during development. The supplier should keep a decision log, return marked drawings, identify the owner of open actions and distinguish confirmed dates from estimates. Ask how material or process substitutions are escalated, how reference samples are retained and how a repeated order is matched to the previous revision. Clear communication does not prove manufacturing performance by itself, but poor document control before an order is a strong warning that the same ambiguity may continue during production.
Coin programs often combine multiple dates, languages, edition numbers, inserts and certificates. The packaging may be physically identical while the printed identity changes. That makes version control a product-quality issue, not merely a design task.
Assign a unique code and revision to every box, sleeve, label, certificate and insert drawing.
Create a bill of materials that maps each edition to the correct components and quantity.
Approve print-ready artwork and a rendered placement proof; confirm that the structural dieline revision matches the artwork template.
Define who supplies serial data, how duplicates are prevented and how unused or rejected serialized items are controlled.
Require written approval before changing paper, insert material, adhesive, foil, carton configuration or production site when the change may affect appearance or performance.
Keep approval evidence together: signed physical sample, final drawing, artwork PDF, color or material reference, packing instruction and inspection criteria. A digital filename such as “final-v7-new” is not revision control. The purchase order should name the approved codes, not depend on the newest email attachment.
Send the same RFQ package to each shortlisted supplier and require a line-by-line response. Mark unknown items clearly and ask the supplier to recommend an option with its effect on fit, appearance, price and lead time. Then compare landed scope, risk and evidence, not only the lowest unit number.
Item: capsule, slab or medal sample/drawing; dimensions, weight, count and orientation.
Структура: box style, finished size constraints, insert, removal feature, certificate and accessories.
Appearance: artwork, print, paper, color targets, foil, embossing and visual standards.
Количество: total quantity and quantity for every artwork, language or edition.
Sampling: required stages, number of samples, approval method and courier destination.
Quality: critical dimensions, defect definitions, inspection or sampling plan and required records.
Packing: unit protection, carton quantity, dividers, carton marks and pallet requirements.
Delivery: destination, required date, shipment mode and Incoterm version.
Quote return: materials, unit price breaks, tooling, sample cost, packing, validity, exclusions and assumptions.
Incoterms allocate defined delivery obligations, costs and risks between buyer and seller; they do not replace your product specification, payment terms or quality agreement. Use the exact named place and agreed rule, and confirm responsibilities using the official ICC Incoterms resources.
Before award, close every open assumption, approve the sample path and record the change-control rule. A purchase order should reference the controlled specification and state what happens if material availability, artwork, quantity or delivery timing changes. This is the point at which sourcing becomes a repeatable production program rather than a one-time visual purchase.
Send the actual capsule or controlled drawing, certificate size, preferred structure, artwork, quantity by edition, destination and acceptance criteria. GPLPAK can review the brief and define the appropriate structural and production-intent sample steps.
© 2026 ГПЛПАК — Custom Paper Packaging Manufacturer in China
 Горячие новости
2026-09-23
2026-09-22
2026-09-21
2026-09-18
2026-09-17
2026-09-17
2026-09-16
2026-09-09
2026-08-31
2026-08-26
Discover premium packaging solutions from Dongguan Xinglan Packaging Products Co., Ltd. Specializing in innovative, durable, and custom packaging products for diverse industries.
GPLPAK стремится к обеспечению высочайшего уровня производственной деятельности.