 EN
 EN
 RU
 ES
 KO
 JA
 PT
 IT
 DE
 FR
 NL
Enlaces rápidos
In brief: custom cinnamon roll packaging boxes are made-to-order paperboard or corrugated packs sized around the finished, decorated pastry, its liner, the number of rolls and the intended sales route. The correct specification protects icing clearance, supports the loaded base, manages grease or condensation for the declared use, carries required information and remains practical for bakery staff to erect and close.
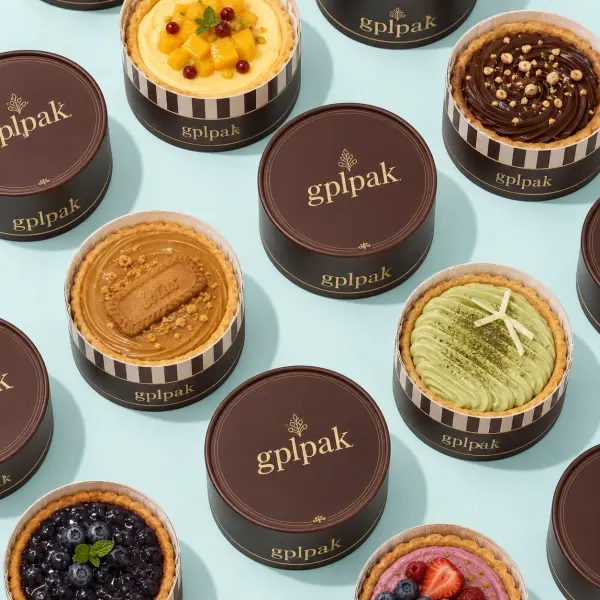
A stock pastry box can be adequate for short counter service, but wholesale buyers usually need a repeatable specification that works across production, packing, retail display and delivery. That specification cannot be chosen from nominal roll count alone. A heavily frosted four-pack may require more headspace and a stronger base than six small rolls, while a refrigerated retail pack has different material and labeling needs from a warm takeaway order.
This guide focuses on B2B custom manufacturing rather than ready-made consumer containers. It explains what to measure, how common box structures differ, where food-contact responsibilities begin, which print decisions affect converting, how to approve a sample and what information produces a comparable wholesale quotation.
The phrase “cinnamon roll packaging” can describe four different things: a counter-service carton, a printed secondary box, a distribution shipper or an insulated system. These packages do not prove the same performance. A branded folding carton can organize and present the pastry, but it does not automatically provide validated temperature control or distribution protection. An outer corrugated case can improve transport strength, but it does not determine whether the surface touching the roll is suitable for food contact.
| Package layer | Primary job | Typical form | What it does not prove |
|---|---|---|---|
| Direct-contact component | Separates the pastry from other materials | Paper liner, cup or tray | Strength of the complete retail pack |
| Retail or takeaway box | Holds, presents and identifies rolls | Folding carton or microflute box | Temperature control or courier qualification |
| Distribution pack | Protects multiple retail packs in transit | Corrugated case with dividers | Food-contact suitability of the inner pack |
| Thermal system | Maintains a defined temperature profile | Insulation, refrigerant and outer shipper | Performance beyond its tested payload and route |
Start the brief with the sales route: bakery counter, local delivery, refrigerated retail, catering, corporate gifting or parcel shipment. Then define whether the requested item is the food-contact surface, the branded secondary box, the outer shipper or a complete pack system. This one distinction prevents a visually attractive carton from being approved for a job it was never engineered to perform.
The distinction also makes supplier quotations more comparable. If one converter quotes only a printed retail carton while another includes a liner, divider and export case, the lower unit price may represent a smaller scope rather than a more efficient offer. Ask each supplier to identify every supplied component, its material, the delivered condition and who assembles it. Flat-packed cartons reduce freight volume but move erection labor to the bakery or co-packer; pre-assembled packs reverse that tradeoff.
For most bakery programs, structure selection is a balance between protection, packing speed, flat-storage efficiency, printing area and delivery strength. The following options are starting points, not universal prescriptions. The final choice should be checked with the actual product, liner and pack-out method.
| Estructura | Best fit | Operational advantage | Approval focus |
|---|---|---|---|
| Tuck-top folding carton | Single roll or small takeaway pack | Ships flat and provides broad printable panels | Closure force, topping clearance and base stiffness |
| Auto-lock or crash-lock carton | Higher-volume counter packing | Faster base setup and improved loaded-base support | Folding sequence, glue joint and line speed |
| Microflute corrugated box | Heavier multipacks, catering and delivery | More edge and stacking strength than light carton board | Freight cube, print method and outer case fit |
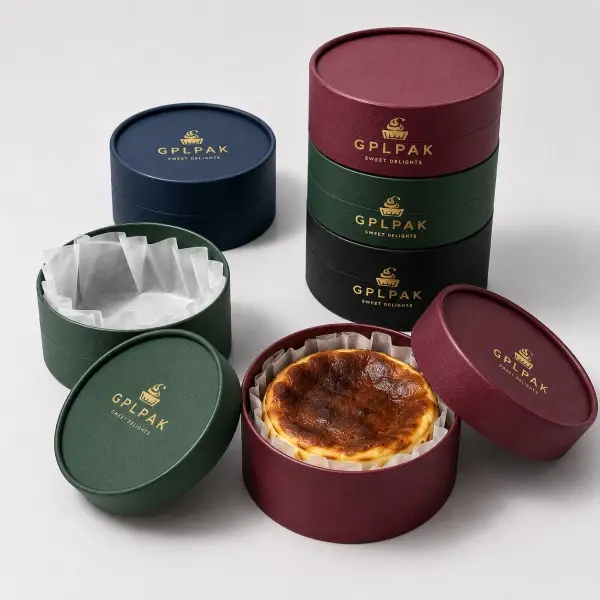
| Lid-and-base presentation box | Premium gifting or limited editions | Controlled reveal and a strong branding surface | Food-contact liner, assembly labor and shipping volume |
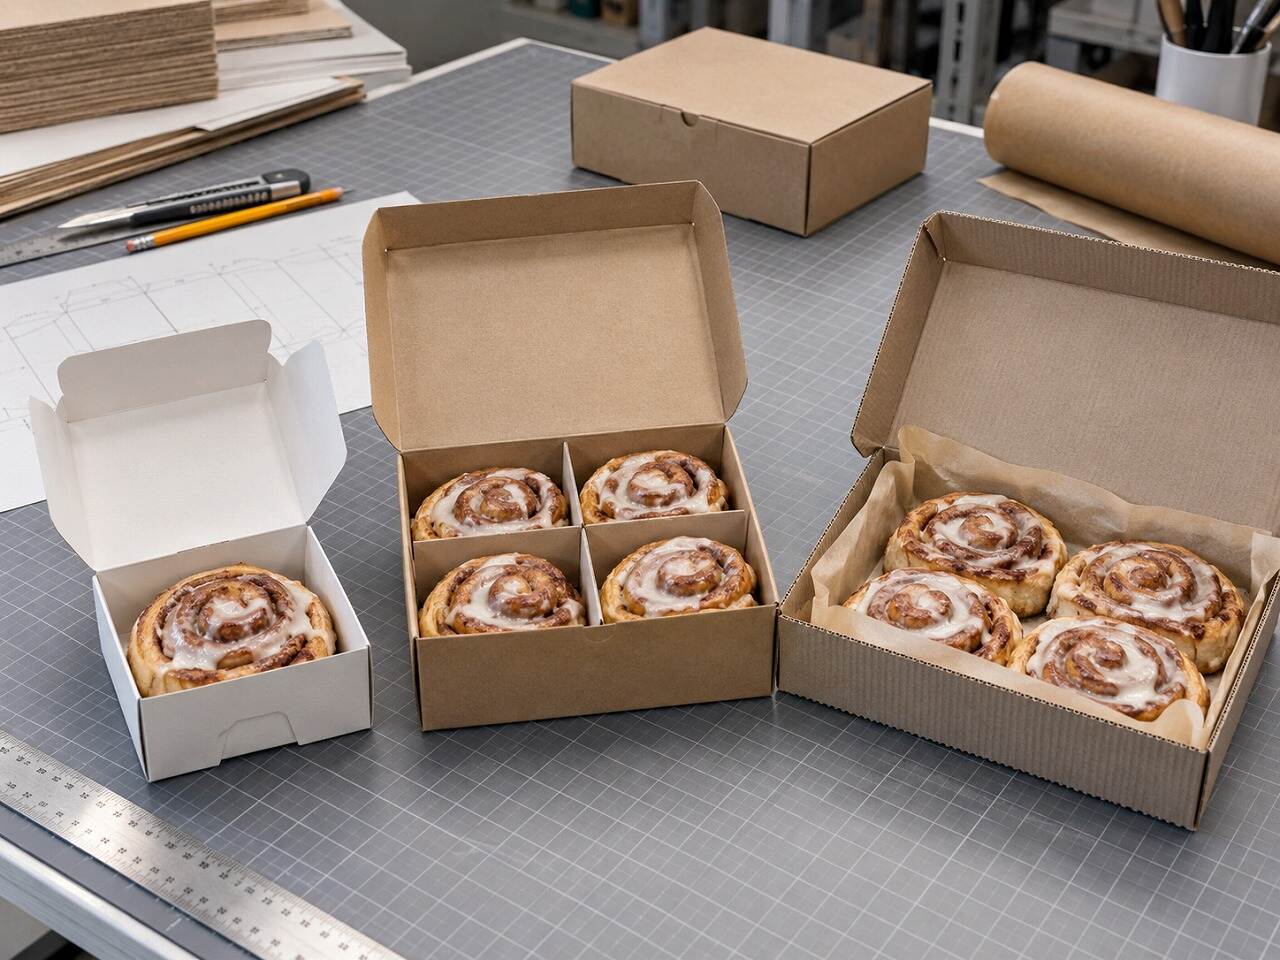
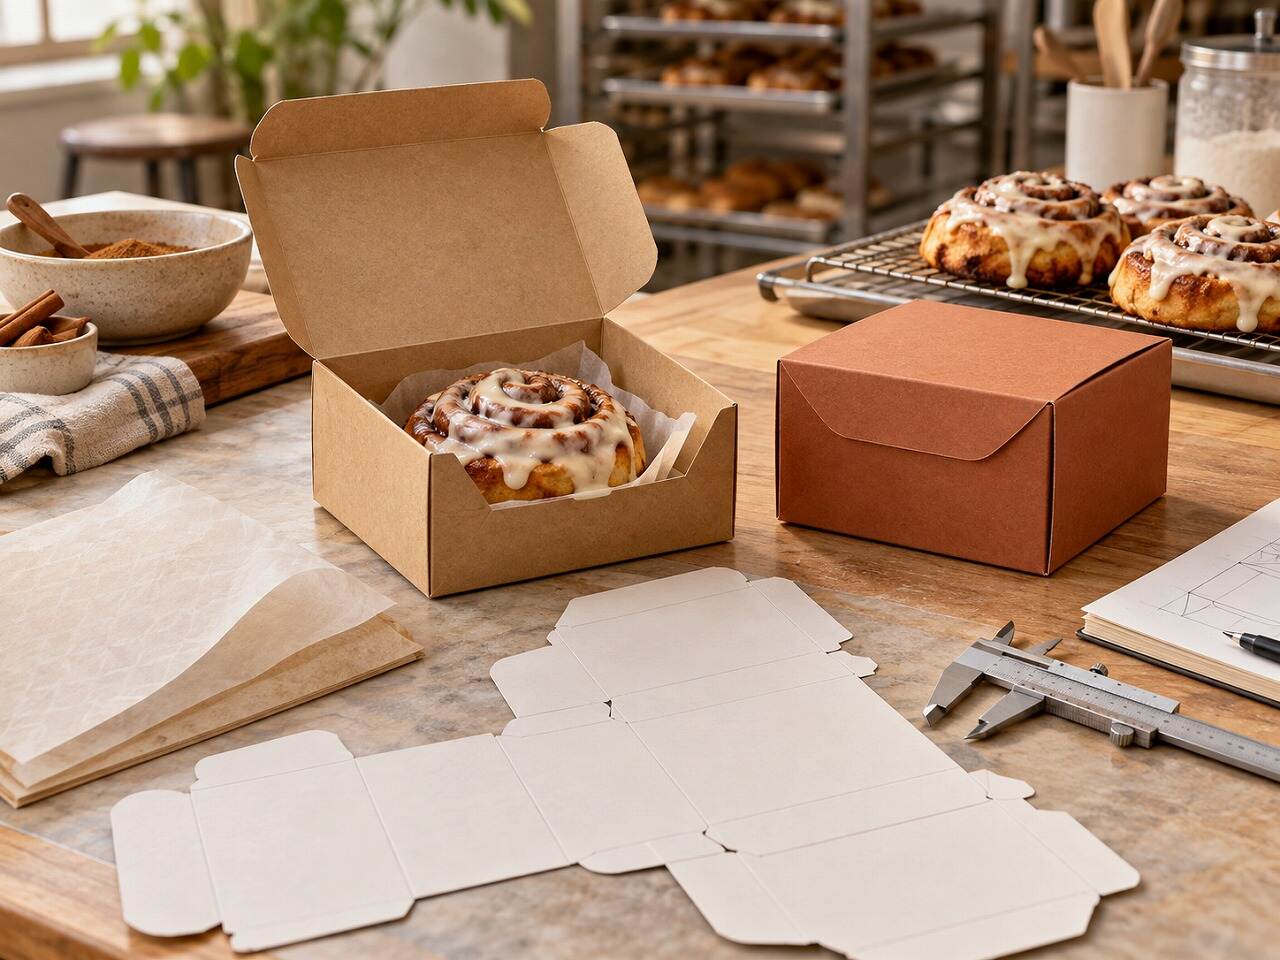
Physical prototypes make pack-count, divider and stacking decisions easier to evaluate than a flat dieline alone.
A window is a configuration rather than a separate box style. It can be added to several structures, but the opening removes paperboard from the panel and can alter stiffness. Window size, film, adhesive, fogging, label space and end-of-life claims therefore belong in the same specification as the box, not in a late artwork note.
Structure should also match the bakery's packing operation. A manual counter team may prefer a simple one-piece carton with an intuitive closure, while a central kitchen may value a pre-glued base that opens quickly and behaves consistently at higher throughput. Request an assembly trial with the people who will actually pack the rolls. Measure whether the carton stays open during loading, whether closures catch on gloves or liners, and whether the packed box can be picked up without the base flexing.
Do not size a custom cinnamon roll box from nominal dough weight or an undeclared “standard roll” diameter. Measure the maximum finished envelope after baking, cooling and decorating. Include the tallest icing peak, toppings that can move, the paper cup or tray, and any tolerance created by normal production variation. If several flavors share one structure, test the largest production-representative sample.
Maximum finished diameter and height
Unit weight and number of rolls
Icing, glaze, butter and topping condition
Cup, liner, tray or divider dimensions
Packing temperature and cooling stage
Loading direction and staff assembly method
Stack height and carry orientation
Storage time and distribution route
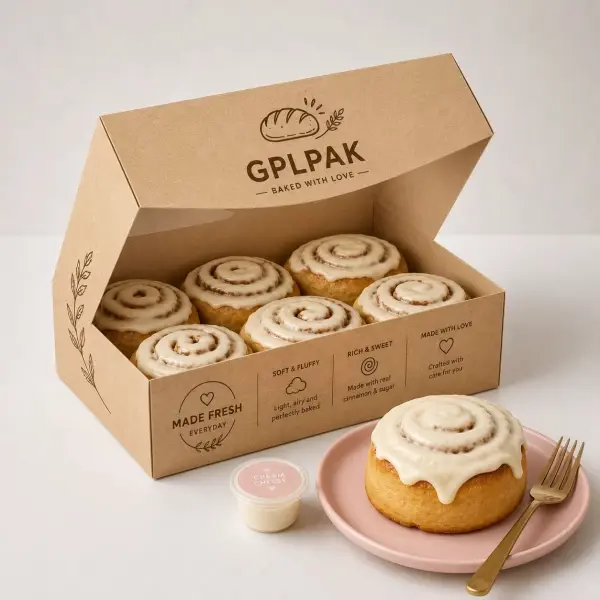
Headspace is a functional clearance, not a universal allowance. Too little clearance transfers icing to the lid; too much clearance allows movement and can increase material and freight cube. For multipacks, test removal as well as fit: a roll may sit securely yet be difficult to lift without touching the surrounding pastries. Finger access, divider height and liner stiffness all affect the customer experience.
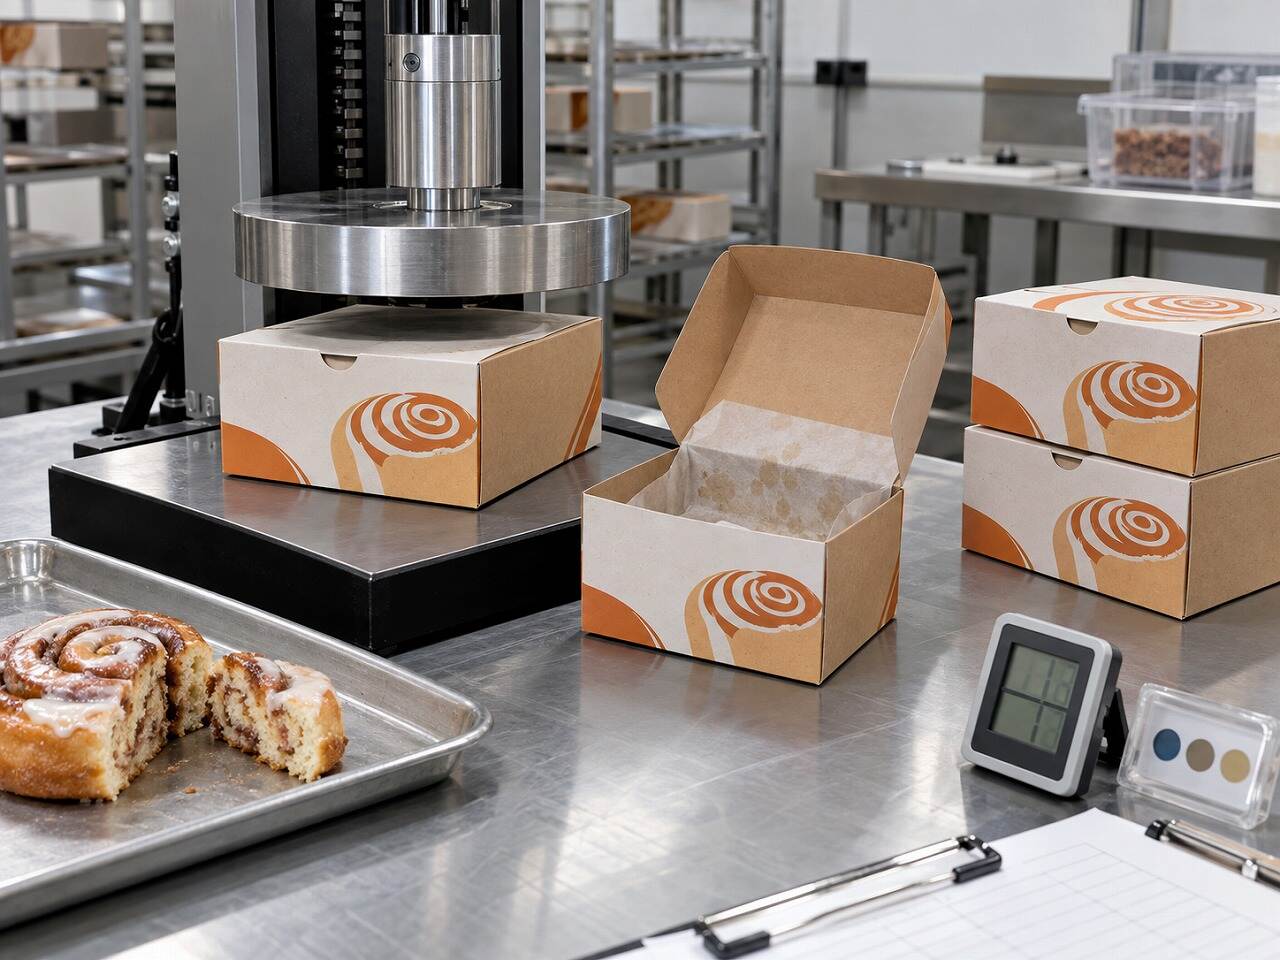
Compression, grease contact and holding-condition checks should use the actual product and intended pack-out—not an empty carton alone.
Buyer action: send a physical product sample when possible. If that is impractical, provide a controlled drawing with maximum dimensions, photographs from the top and side, product weight, liner dimensions and the measurement method used.
Material selection begins with the contact condition. A roll placed directly against the box creates a different requirement from a roll held in a separately qualified cup, liner or tray. The finished article may combine paperboard, coating, ink, varnish, adhesive, window film and an insert. Suitability must be assessed for the relevant components, food type, temperature, duration and destination market.
| Material system | Useful characteristic | What the buyer must confirm |
|---|---|---|
| White folding boxboard or SBS | Smooth surface for detailed printing | Grade, caliper, barrier and contact status |
| Kraft paperboard | Natural visual character | Color reproduction and grease management |
| Microflute corrugated board | More structural support for heavier loads | Flute, liner combination, print process and case fit |
| Separate liner, cup or tray | Defines the food-contact surface and contains grease | Material declaration, fit, removal and disposal route |
“Grease-resistant” describes a performance need; it does not by itself establish food-contact compliance. The U.S. Food and Drug Administration explains that the regulatory status of a food-contact material depends on its component substances and intended use. The European Commission identifies Regulation (EC) No 1935/2004 as the general framework for food-contact materials in the European Union. Buyers should request current documentation for the exact material configuration rather than rely on a generic “food-grade” logo.
Documentation should name the material or component covered and the conditions for which the statement applies. A declaration for the base paper does not automatically cover a printed, coated and glued finished box. Likewise, a material that is suitable for dry food at ambient temperature may not support a different contact condition without additional evidence. Your regulatory or food-safety team should review the supplier documents against the actual product, process and market before the commercial artwork is released.
Compliance boundary: printing, coatings, adhesives and grease-resistant treatments should be reviewed for the declared contact condition. Do not publish “PFAS-free,” recyclable, compostable or food-safe claims until the complete material system and supporting evidence have been checked for the destination market.
FDA food-contact material status · FDA PFAS food-contact update · EU food-contact legislation
Artwork should be built on the approved production dieline, not on a generic mockup. Keep logos, barcodes, ingredients, allergen statements and legal copy away from cut edges, scores, glue flaps and window openings. The bakery or food brand remains responsible for the accuracy and legal sufficiency of product information in its destination market; the converter is responsible for reproducing the approved artwork and agreed packaging specification.
Useful for photography, gradients and multi-color graphics. Approve image resolution, proofing method and total coverage.
Useful for brand-critical solid colors. Supply a physical color target and account for substrate influence.
Varnish or an appropriate coating can help manage rubbing and handling. Confirm appearance and contact boundary.
Improves product visibility but changes panel stiffness. Confirm film, adhesion, fogging and label area.
Premium finishes such as foil or embossing can support a gift program, but they add tooling, process steps and inspection points. They also should not distract from closure reliability, grease control and readable product information. For a high-volume bakery line, consistent print, accurate scoring and fast erection often create more operational value than a decorative effect applied before the structure is proven.
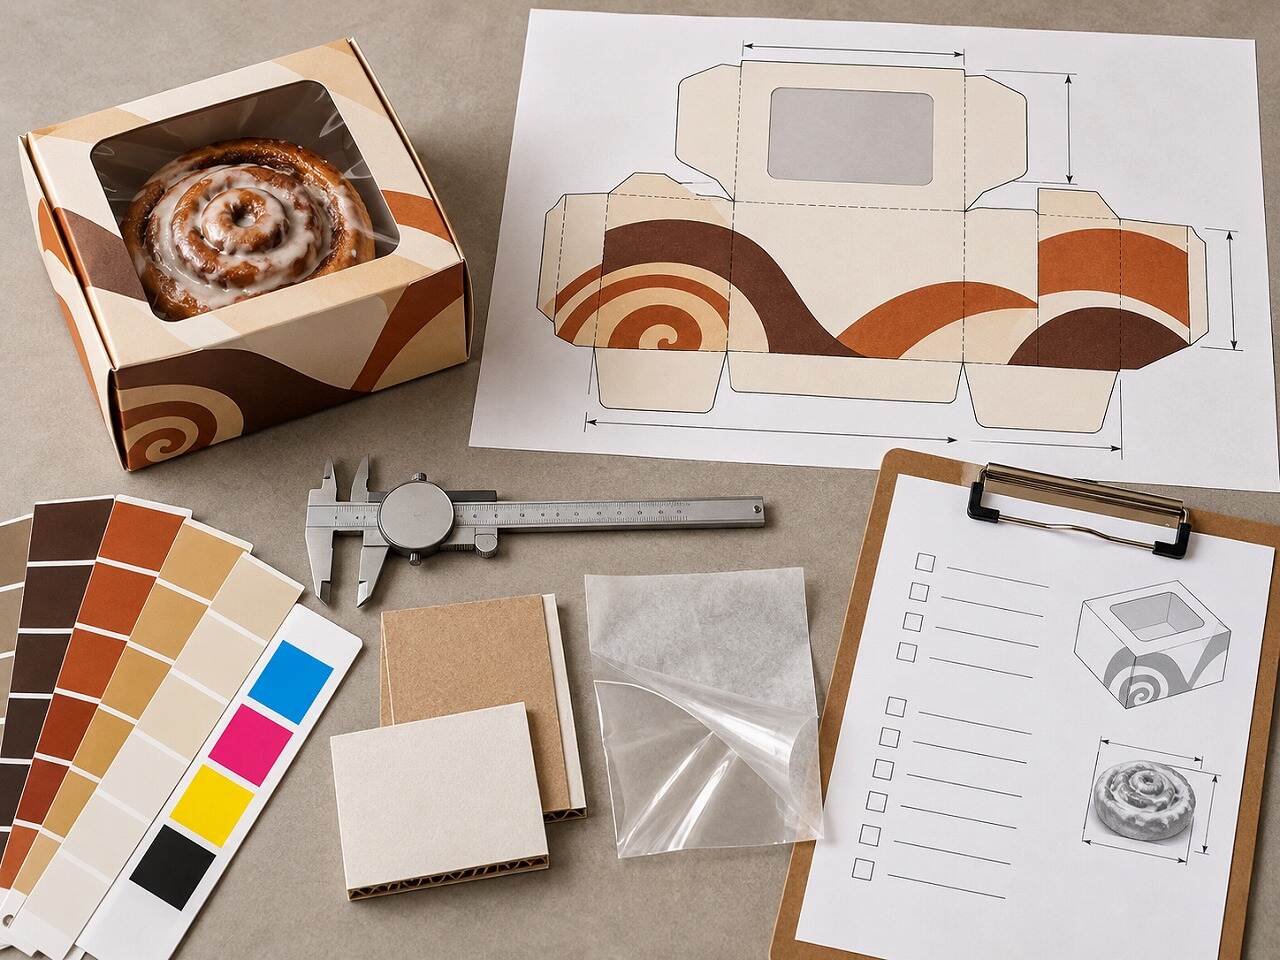
A controlled RFQ should connect the dieline, material, barrier, window, print target and acceptance checklist in one specification set.
Warm cinnamon rolls create a process question rather than a simple material question. Steam can condense inside a closed pack, soften paperboard, affect window clarity and alter icing or product texture. Ventilation can release moisture, but it may also change heat loss, aroma retention and product drying. The food producer should therefore validate cooling time, packing temperature, venting and holding time with the actual recipe and route.
Local delivery adds vibration, tilting, stacking and rider handling. Test the retail box inside the real delivery bag or outer case. A box that performs well on a counter may slide when stacked in a vehicle. For heavier multipacks, check base deflection, corner crushing and closure retention at the maximum intended load. If parcel shipment is planned, treat the branded box as an inner package and engineer a separate transport system.
Pack rolls at representative temperature and record the cooling interval.
Hold the closed pack for the intended dwell time and inspect condensation, staining and board softness.
Stack loaded boxes to the proposed height and observe base and lid deformation.
Run the actual carry or delivery orientation, including stops and turns.
Document acceptance criteria before repeating the test with production material.
A rendering can show graphic direction, but it cannot confirm fit, assembly speed, odor, board behavior, grease resistance or closure performance. Use samples in stages. Begin with an unprinted structural prototype to approve dimensions and loading. Move to a decorated sample only after the structure is stable. GPLPAK's muestreo de desarrolloydesign validation pages describe how physical samples and production-readiness review can support approval before mass production.
| Approval stage | What it should prove | Record before approval |
|---|---|---|
| Blank prototype | Fit, headspace, loading, closure and removal | Internal dimensions, board and structural revision |
| Decorated sample | Artwork direction, color, finish and window placement | Artwork revision, proof reference and finish standard |
| Packed-use trial | Grease, condensation, handling and stacking behavior | Product condition, temperature, duration and pass criteria |
| Mass-production inspection | Conformance to the signed specification | Sampling plan, tolerances and defect definitions |
Useful acceptance criteria include dimensions and tolerances, print reference, score quality, glue placement, closure function, window adhesion, rub resistance and any agreed grease-resistance evaluation. Avoid approving a sample only as “looks good.” A signed sample is most useful when it is tied to a written bill of materials, artwork version and measurable requirements.
For production inspection, distinguish critical, major and minor defects in language relevant to the pack. Contamination, unsafe sharp edges or an incorrect food-contact component may be treated differently from a visible glue mark or a small color deviation. Define the sampling plan, inspection lighting, measurement tools and decision authority before shipment. When a deviation is found, the supplier and buyer should be able to trace it to the applicable requirement instead of debating an undefined visual expectation.
There is no responsible universal MOQ or unit price for custom cinnamon roll packaging. Economic quantity depends on the dieline, dimensions, board yield, print process, barrier system, window, insert, number of artwork versions and packing method. A quote should separate recurring unit cost from one-time items such as cutting dies, plates or special tooling when those charges apply.
| Cost driver | Why it changes price | Practical buyer action |
|---|---|---|
| Finished dimensions | Affect sheet yield, board use and freight cube | Approve the smallest functional size with real product |
| Structure and material | Change converting steps and setup | Compare options against the same performance brief |
| Print and finishing | Add plates, passes, tooling and inspection points | Prioritize brand-critical effects |
| SKU count | Splits quantity across artworks and may repeat setup | Use a shared structure and variable labels where suitable |
| Shipping format | Flat versus assembled packs use different carton volume and labor | Compare landed cost, not unit price alone |
Ask for two or three quantity levels against one controlled specification. This reveals where setup and material efficiency change the unit price. If quotations use different board grades, dimensions, barriers or packing assumptions, they are not directly comparable. MOQ and production timing should be confirmed in the project quotation because capacity, tooling and material availability can change.
Calculate landed cost at the point where the bakery will use the packaging. Include unit packing, master cartons, pallets, freight, import charges where applicable, storage space, assembly labor and expected waste. A slightly more expensive flat carton may reduce storage and transport cost; a pre-glued structure may cost more to ship but save packing time. The right comparison depends on your labor rate, order frequency, warehouse constraints and service level, not on ex-factory unit price alone.
Forecast discipline matters as well. Sharing annual demand, order cadence and SKU mix allows a converter to discuss material purchasing and production planning without turning an uncertain forecast into a contractual commitment. Keep safety stock and seasonal peaks visible in the planning model, especially when a printed pack contains date-specific campaigns or promotional artwork that cannot be reused later.
A strong supplier response begins with a strong request for quotation. State the package layer, finished product measurements, pack count, contact configuration, sales route and destination market. If the structure is not fixed, request alternatives against the same acceptance criteria rather than asking for “the cheapest cinnamon roll box.” GPLPAK's packaging consultationyproduct development pages outline early-stage support available before sampling.
Maximum roll dimensions, weight and photographs
Number and arrangement of rolls per box
Direct or indirect food-contact configuration
Preferred structure, window, liner or divider
Quantity by SKU, destination and required date
Material and structural specification
Relevant food-contact documentation
Sample type and what it will prove
Unit packing, master carton and delivery assumptions
MOQ, tooling, production timing and quote validity
Evaluate suppliers on their questions as well as their answers. A capable converter should ask about the finished pastry, contact surface, packing temperature, route and approval criteria before recommending a material. Warning signs include substituting a generic mockup for a physical fit sample, making blanket compliance claims without identifying the material configuration, or quoting an unusually low price against an incomplete specification.
The final purchase order should reference the approved dieline, artwork revision, material description, color standard, finish, packing method and sample or inspection criteria. Record how future changes will be controlled. A new board mill, coating, adhesive, window film or production site can affect fit, appearance or documentation even if the outer design appears unchanged. Requiring written approval for material or process substitutions helps preserve consistency across repeat orders.
Send the finished roll dimensions, pack count, contact configuration, artwork status, order quantity and destination. GPLPAK can review the structure, material, printing and sampling path and prepare a project-specific quotation.
© 2026 GPLPAK · Custom paper packaging manufacturer · Dongguan, China
 Noticias Calientes
2026-10-07
2026-09-30
2026-09-23
2026-09-22
2026-09-21
2026-09-18
2026-09-17
2026-09-17
2026-09-16
2026-09-09
Discover premium packaging solutions from Dongguan Xinglan Packaging Products Co., Ltd. Specializing in innovative, durable, and custom packaging products for diverse industries.
GPLPAK está comprometido con la excelencia en la manufactura.